Why Us?
For over 30 years, Taifitop has been at the forefront of water treatment innovation, delivering cutting-edge, chemical-free solutions that redefine efficiency, sustainability, and reliability.
From industrial giants to everyday homes, our pioneering QEQI® technology is trusted worldwide to optimise water systems, reduce maintenance costs, and protect the environment.
The Pioneer in Physical Water Treatment
Our commitment to continuous research and innovation has refined our solutions, ensuring they meet the evolving needs of diverse industries. QEQI® is now used worldwide, from residential homes to large-scale industrial applications, with a proven track record of delivering reliable, sustainable results.
What Makes QEQI® Different?
A scientific and research-driven approach
Built on decades of rigorous scientific research, QEQI® uses high-frequency electromagnetic waves to treat water without chemicals, providing proven and sustainable solutions.
Commitment to Integrity
At QEQI®, we lead with innovation and integrity. Unlike imitators, our technology is backed by decades of research, ensuring genuine, high-quality, and proven water treatment solutions you can trust.
Proven ROI
QEQI® ensures measurable returns on investment by significantly reducing energy costs, extending equipment lifespan, and lowering maintenance expenses. Its long-term efficiency guarantees that every pound spent delivers valuable savings.
Effortless Installation & Universal Compatibility
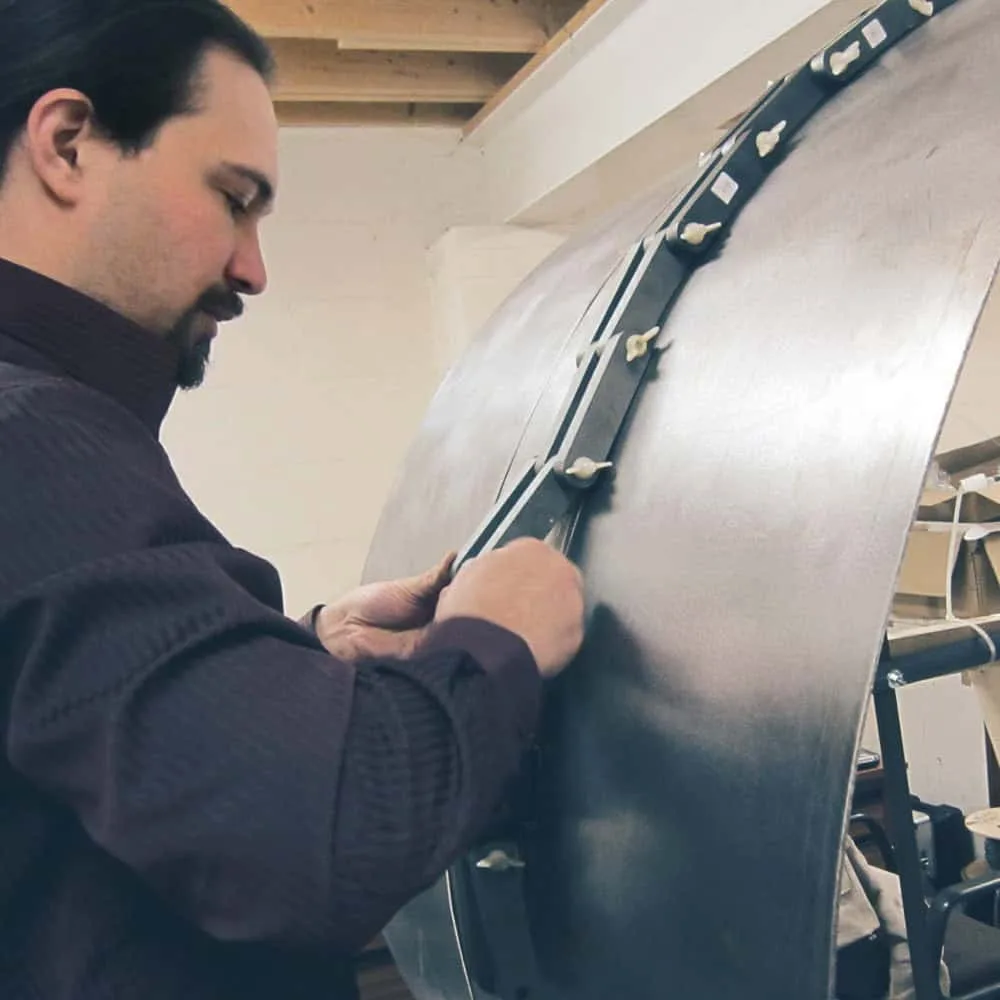
QEQI® operates efficiently, regardless of water flow rate or pipe material. With its innovative design, installation is seamless, no retrofitting, no pipe cutting, just a simple, non-intrusive fit-and-forget solution that starts working immediately.
Sustainability at the Forefront
At QEQI®, we prioritise sustainability. Our technology helps reduce energy consumption, extends the lifespan of equipment, and lowers the carbon footprint, making it an eco-friendly choice for both businesses and the environment.
Proven Durability and Longevity
Although our systems come with a 3-year warranty, many units have reliably run for over 15 years, ensuring long-term savings on replacements and maintenance. This proven durability demonstrates QEQI®’s ability to provide lasting value and performance for your systems.
The Science Behind QEQI® Technology
QEQI® uses a patented electromagnetic signal that induces an electric field into the pipe and fluid within. By utilising transformer technology, it ensures maximum efficiency while operating on all pipe materials, even those with insulation. The system requires no physical contact with the pipe, and it is not sensitive to alignment. The signal is transmitted throughout the entire pipe network, preventing scale formation, removing existing scale, controlling biofilm, and mitigating corrosion.
For a more detailed explanation of this process, please click the button below.
Versatility: One Solution for All Applications
Agriculture Industry
- Treats limescale in irrigation and greenhouse heating systems.
- Maintains flow in drip lines and fertigation units.
- Reduces blockages and improves water efficiency in farming operations.
COMMERCIAL HEATING AND COOLING INDUSTRY
- Protects HVAC systems, water heaters, and plate heat exchangers.
- Improves energy efficiency and reduces call-outs.
- Supports sustainable building management strategies.
Cooling Tower Industry
- Treats limescale in evaporative cooling systems and heat exchangers.
- Reduces blowdown and water wastage.
- Improves energy efficiency and extends cooling equipment lifespan.
FOOD INDUSTRY
- Treats limescale in dishwashers, steam ovens, and processing equipment.
- Ensures consistent operation and hygiene in production environments.
- Reduces cleaning costs and equipment downtime.
HOTEL INDUSTRY
- Treats limescale in guest room boilers, kitchens, pools, and spas.
- Enhances guest comfort and reduces service interruptions.
- Reduces water heating costs and extends appliance life.
Marine INDUSTRY
- Treats limescale in seawater and potable water systems onboard.
- Protects desalinators, HVAC systems, and galley equipment.
- Reduces cleaning requirements and improves operational efficiency.
MINING INDUSTRY
- Treats limescale in high-solid process water, pumps, and pipelines.
- Reduces equipment wear and maintenance in harsh environments.
- Supports uninterrupted production in mineral extraction.
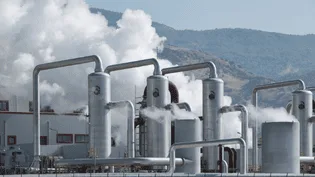
STEAM PRODUCTION INDUSTRY
- Treats limescale in boiler tubes, condensate return lines, and heat exchangers.
- Improves steam quality and energy efficiency.
- Reduces maintenance, blowdown, and chemical costs.
Swimming Pool INDUSTRY
- Treats limescale in heaters, filters, and water features.
- Reduces staining on tiles and surfaces.
- Improves water clarity and reduces chemical demand.
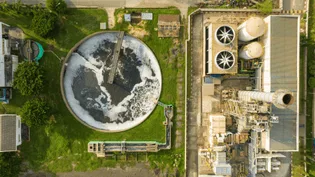
WASTEWATER INDUSTRY
- Treats limescale in sludge heating systems and filtration units.
- Improves flow rates and reduces chemical cleaning.
- Supports sustainable wastewater treatment practices.
Versatility: One Solution for All Applications
| FEATURE | QEQI® | Alternative Solutions |
|---|---|---|
| 📡 Signal Consistency | ✅ Consistent, adaptive signal | ❌ Variable; may weaken fast |
| 💧 Flow Rate Dependence | ✅ Independent of water flow | ❌ Affected by flow changes |
| 🏗️ Material Quality | ✅ High-quality, durable | ❌ Lighter-grade, less robust |
| 🧲 Ferrite Design | ✅ Optimised for efficiency | ❌ Risk of loose assembly |
| 🔌 Electronics & Circuitry | ✅ Advanced, precision circuit | ❌ May lack integrated IC |
| 🛡️ Structural Integrity | ✅ Fixed design for strength | ❌ Moving parts risk wear |
| 🔥 Fire & Heat Resistance | ✅ High quality, fire-resistant materials | ❌ Susceptible to heat damage |
| ⚡ Ease of Installation | ✅ Quick, simple setup | ❌ Extra assembly steps needed |